Integrated modern
plastic products factory
plastic products factory
The information comes from: Internet Published on: 2022-11-07
Reasons and solutions for the frequent breakage of mainstream water outlets in plastic products
The sprue sleeve, also known as the main sprue liner or nozzle, is a channel for molten plastic to enter the mold cavity, connecting the injection molding machine and the mold The sprue sleeve and the injection nozzle of the injection machine are in the same central position
The material head inside the sprue sleeve is broken and difficult to remove
In terms of molds
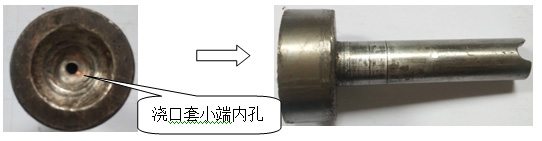
first,The small end inner hole of the sprue sleeve is deformed
Reason: Due to the frequent impact of the nozzle on the curved surface of the sprue sleeve, the small port is concave and prone to buckling
Countermeasure: Use a conical steel file to trim the small port mouth
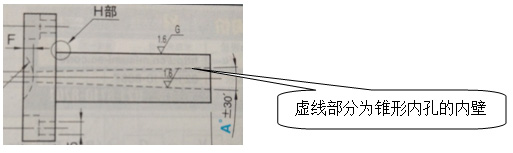
second,The conical inner hole of the sprue sleeve has a reverse buckle
Reason one: Sometimes due to human factors, the inner wall of the conical inner hole may be damaged when removing the material head, resulting in a reverse buckle
Countermeasure one: Use a conical steel file to trim the inner hole and polish it with sandpaper or replace it with a new sprue sleeve
Reason two: After the material ejector pin breaks or deforms, it hits the inner wall of the conical inner hole, causing it to snap back
Countermeasure two: Trim the inner hole with a conical steel file and polish it with sandpaper or replace it with a new sprue sleeve
Reason three: There are material attachments or foreign objects on the inner wall of the conical inner hole
Countermeasure three: Clean the inner wall of the conical inner hole of the sprue sleeve and polish it
third,The smoothness of the conical inner hole of the sprue sleeve is insufficient
Reason: Organic processing marks on the conical inner hole have not been polished properly or have been eroded by materials or gas corrosion
Countermeasure: Use a conical steel file to trim the inner hole and polish it with sandpaper or replace it with a new sprue sleeve
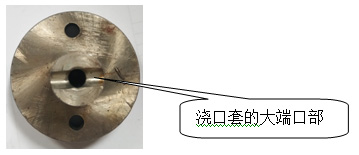
fourth,The large end of the sprue sleeve is deformed
对策:用锥形金钢锉对大端口部进行修整并用砂纸抛光或更换新的浇口套.
fifth,The conical inner hole of the sprue sleeve has cracked
Countermeasure: Replace with a new sprue sleeve
sixth,The sprue sleeve does not match the curved surface of the nozzle
Reason: Due to the mismatch of the curved surface, material leakage occurred, resulting in resistance
Countermeasure: Replace with a new sprue sleeve
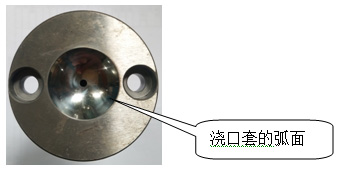
seventh,The sprue sleeve or nozzle arc surface is damaged
Reason: Due to damage to the curved surface causing misalignment, material leakage occurs, resulting in resistance
Countermeasure: Replace the sprue sleeve or nozzle with a new one
eighth,The sprue sleeve and nozzle have different centers
Reason: Due to lack of concentricity, the center of the material head is misaligned, resulting in resistance
Countermeasure one: Adjust the position of the shooting seat up and down, left and right, and keep them in the same center position
Countermeasure two: The clearance between the fixed gate sleeve hole of the mother template and the outer diameter of the gate sleeve is too large. The size of the fixed gate sleeve hole of the mother template should be controlled within 0.1mm
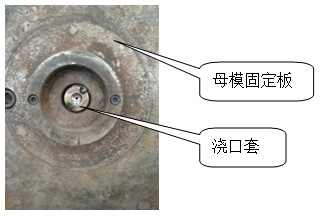
ninth, The inner hole of the small end of the sprue sleeve is smaller than the nozzle hole
Reason: Because the nozzle hole must be 0.5 to 1.0mm smaller than the inner hole of the small end of the sprue sleeve. Otherwise, resistance will be generated during demolding
Reason: Because the nozzle hole must be 0.5 to 1.0mm smaller than the inner hole of the small end of the sprue sleeve. Otherwise, resistance will be generated during demolding
tenth,There is a gap between the outer diameter of the sprue sleeve and the mating hole with the mother mold
Reason: Due to gaps, burrs are generated, which create resistance
Countermeasure: If the sprue sleeve is worn, replace it with a new sprue sleeve or weld the worn part of the sprue sleeve before reassembling
If the inner hole of the mother mold core is worn out, it should be enlarged again and equipped with a new large sprue sleeve, or an insert that matches the sprue sleeve should be machined on the mother mold core
eleventh,The male mold pulled the material and sold it out
Reason: The material pulling pin has the function of pulling and pushing out the material head, and is often subjected to frequent force, which can easily lead to breakage
Countermeasure: Remake a new pull pin and replace it
twelfth, The pulling force of the male mold material sales is insufficient
Reason: When the force of the material pulling pin is insufficient to pull the main gate material head
Countermeasure one: Increase the angle of the material pulling pin and replace it with a new one
Countermeasure two: Process a narrow groove on the male mold core (above the top pin) to hold the main gate material head
Machine aspect
first,Reason: Insufficient cooling time of the product
Countermeasure: Extend the cooling time
second,Reason: Abnormal heating of the heating coil of the nozzle
Countermeasure one: Check if the heating coil wire ends are loose, and if they are loose, fix them again
Countermeasure two: If the heating coil does not heat up, replace it
In addition, incorrect material selection is also a reason for poor material head detachment